Cylindrical plate work
Assess plate forming into cylinders using the target inside diameter, plate width and thickness. Include springback and seam preparation requirements in the process review rather than considering thickness alone.
The upper-roll universal plate rolling machine is assessed for curved and cylindrical plate work. Capacity must be reviewed against material strength, plate width, thickness and the target diameter together. Rolling and pre-bending are separate duties, with end straight allowance, unloading and workpiece support also requiring definition. A stated plate thickness cannot be applied to every diameter or material condition; selection needs the actual part geometry and the intended downstream joining or finishing process.
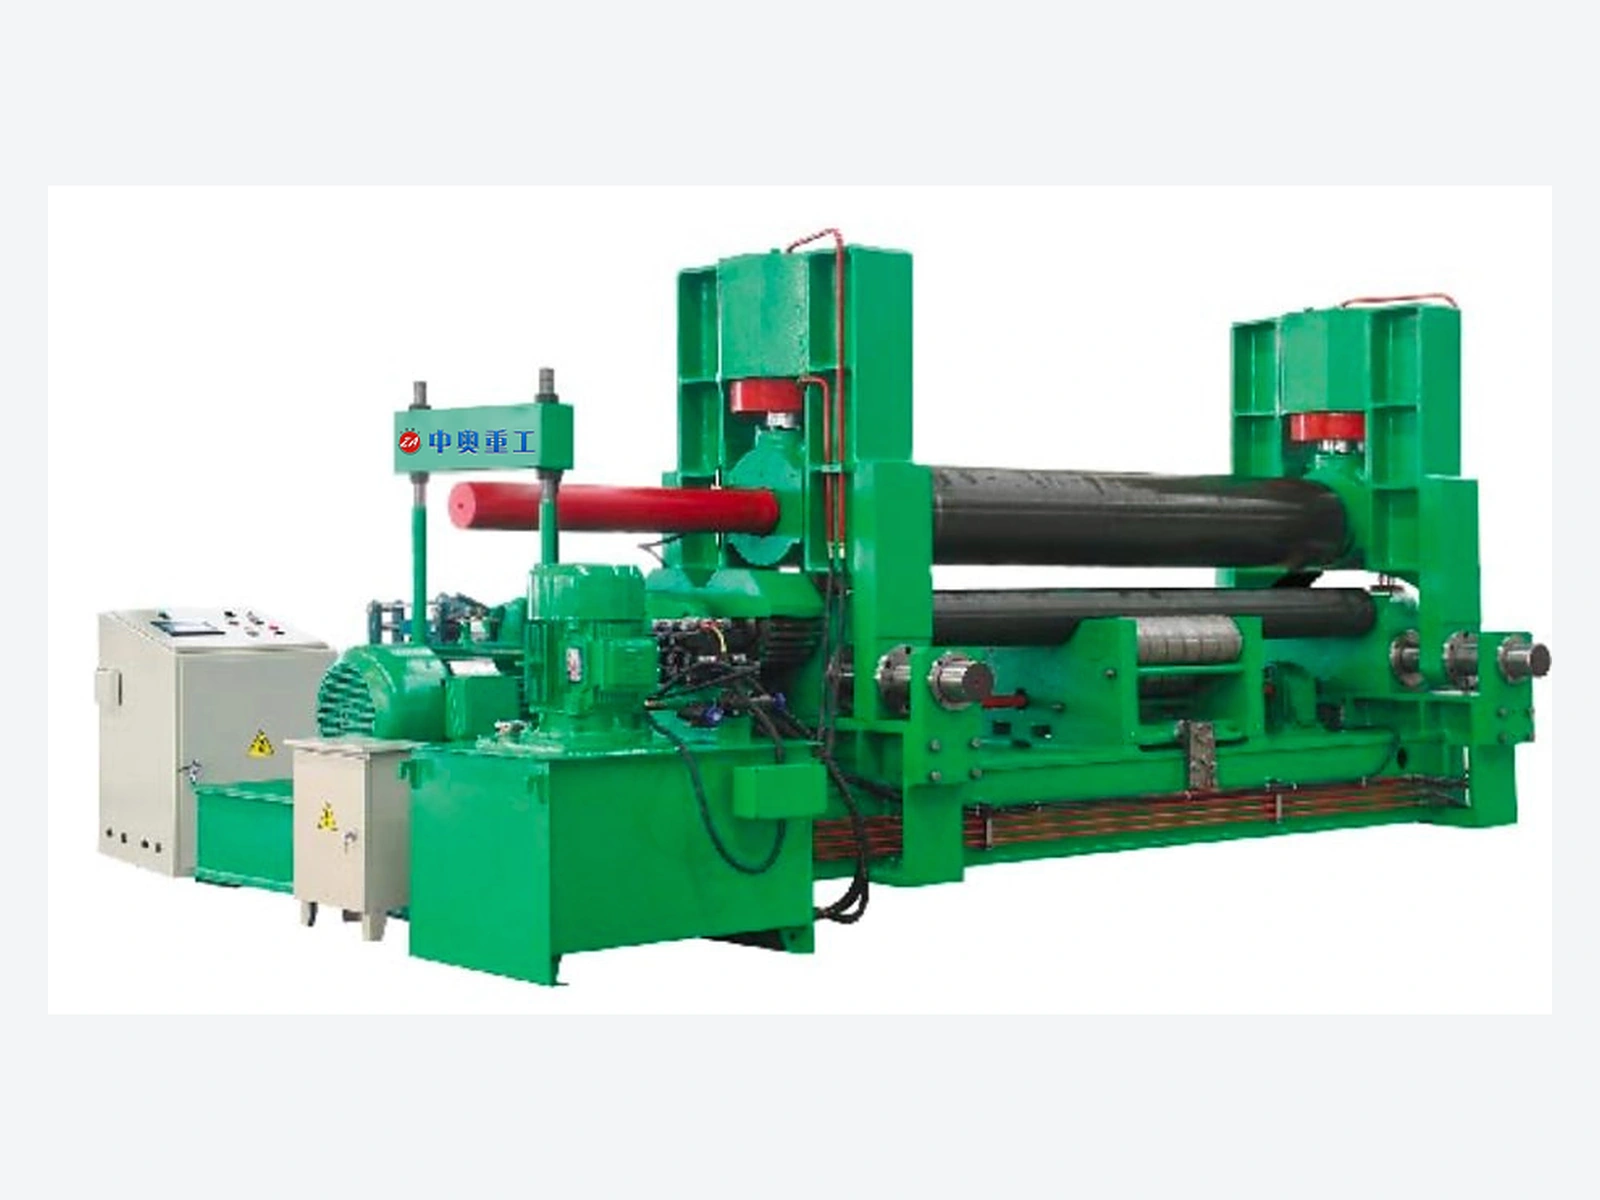
Rolling capacity and pre-bending capacity are different selection points. Review the plate material, width, thickness, target diameter and end-form requirements together.
Roll arrangement, controls, workpiece supports and unloading method are confirmed for the selected machine. Do not assume one plate-thickness rating applies to all diameters or material grades.
Assess plate forming into cylinders using the target inside diameter, plate width and thickness. Include springback and seam preparation requirements in the process review rather than considering thickness alone.
Supply curvature, arc length and end requirements, including whether straight ends are acceptable. Review capability against the material and target radius, with sample arrangements where needed.
Where rolling is followed by fit-up or welding, define end shape, straight allowance and seam requirements. Selection must connect with the next operation rather than rely on finished diameter alone.
Machine photographs illustrate available configurations. Appearance, controller, tooling, protective devices and auxiliary equipment are subject to the agreed supply scope. Final specifications and acceptance requirements are confirmed in the quotation.
Share the information available using the checklist below to help us review the product against your application. If a complete drawing is not available, start with clear photographs and known dimensions.
The button below opens an email with a product-specific checklist. Fill in the details you know and attach drawings or photographs in your email client.
Email a technical enquiryInformation is for initial review, not a commitment on compatibility, supply or performance. Final materials, geometry, configuration, lead time and acceptance requirements are subject to the confirmed drawing and quotation.
Clarify the operating conditions and interfaces before deciding on materials, geometry or configuration.
They require separate confirmation. Target diameter, width, thickness and material strength affect selection together. End pre-bending also involves straight allowance and seam requirements; the two capacities are not interchangeable.
No. Grade, strength, width, target inside diameter or curvature, end requirements and unloading conditions are also needed. The process conditions for one thickness may change with diameter.
Review the equipment, material, pre-bending method and target diameter before defining an end result. Provide the permitted straight allowance, seam drawing and downstream processing needs; no universal zero-straight-end promise is implied.
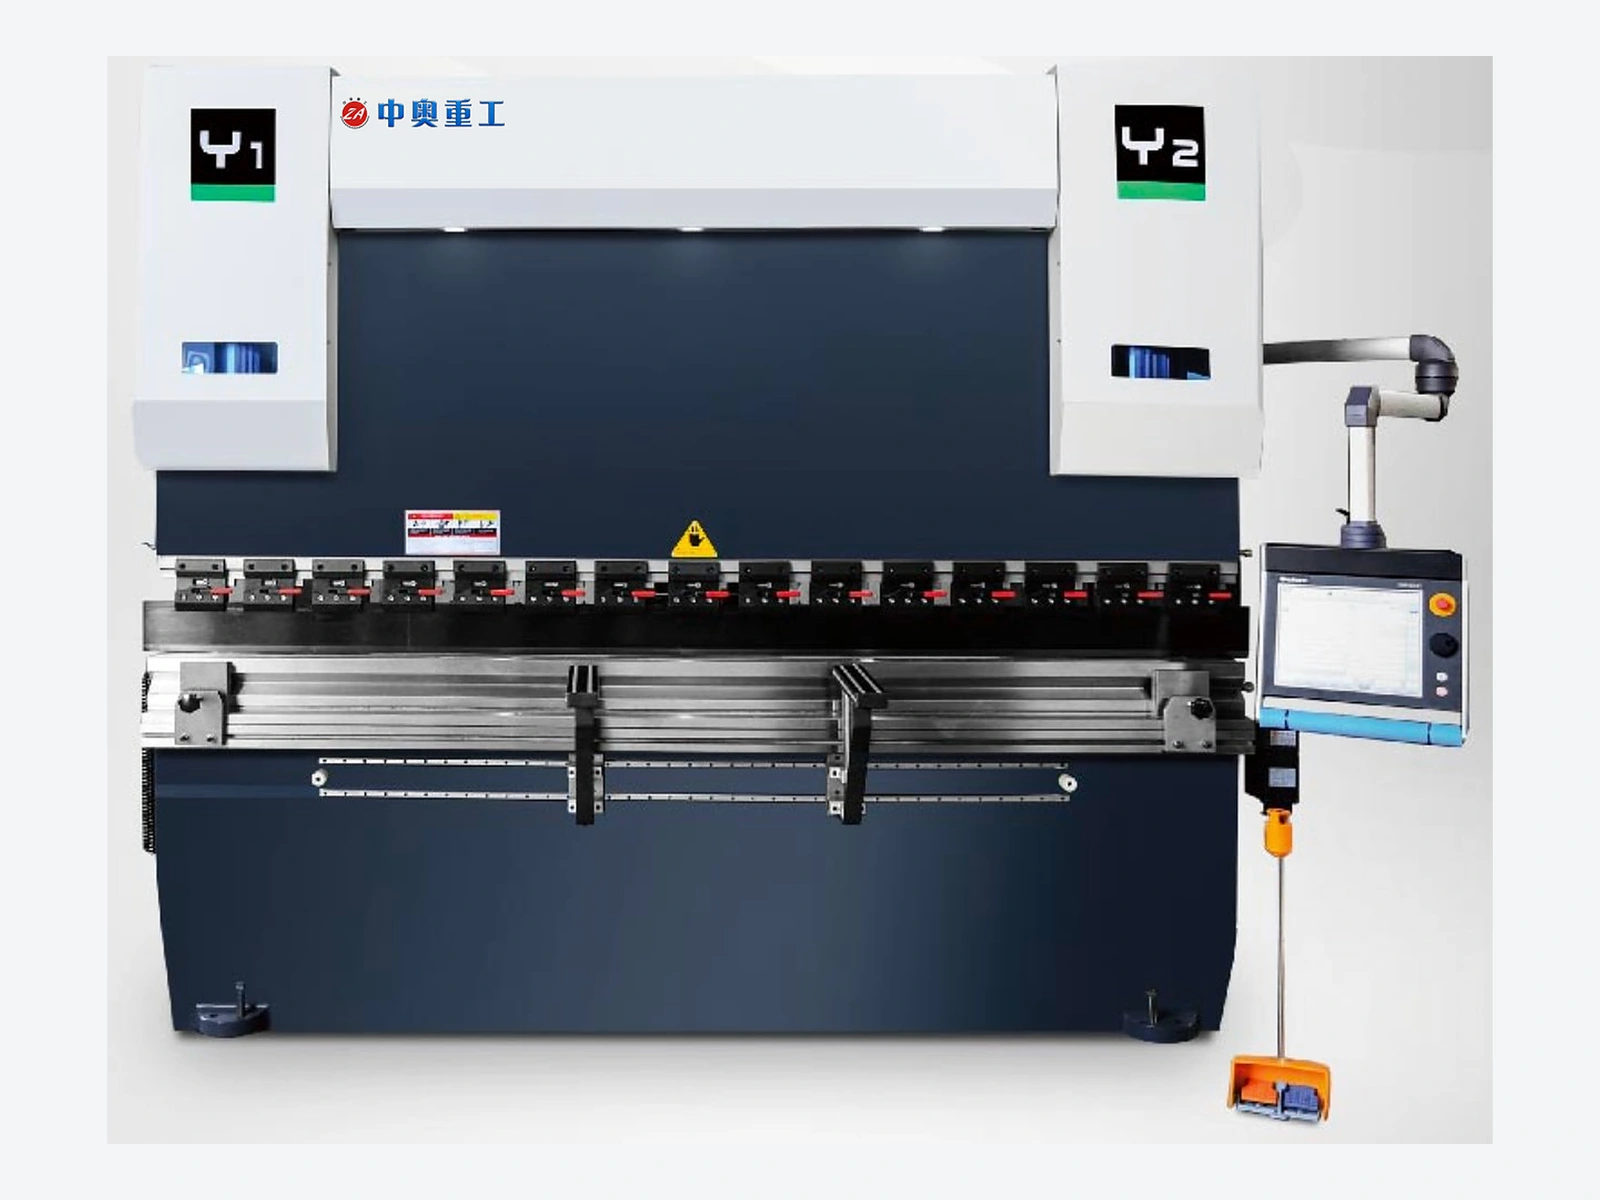
Servo-pump hybrid bending for sheet metal production with application-matched CNC configuration.
View product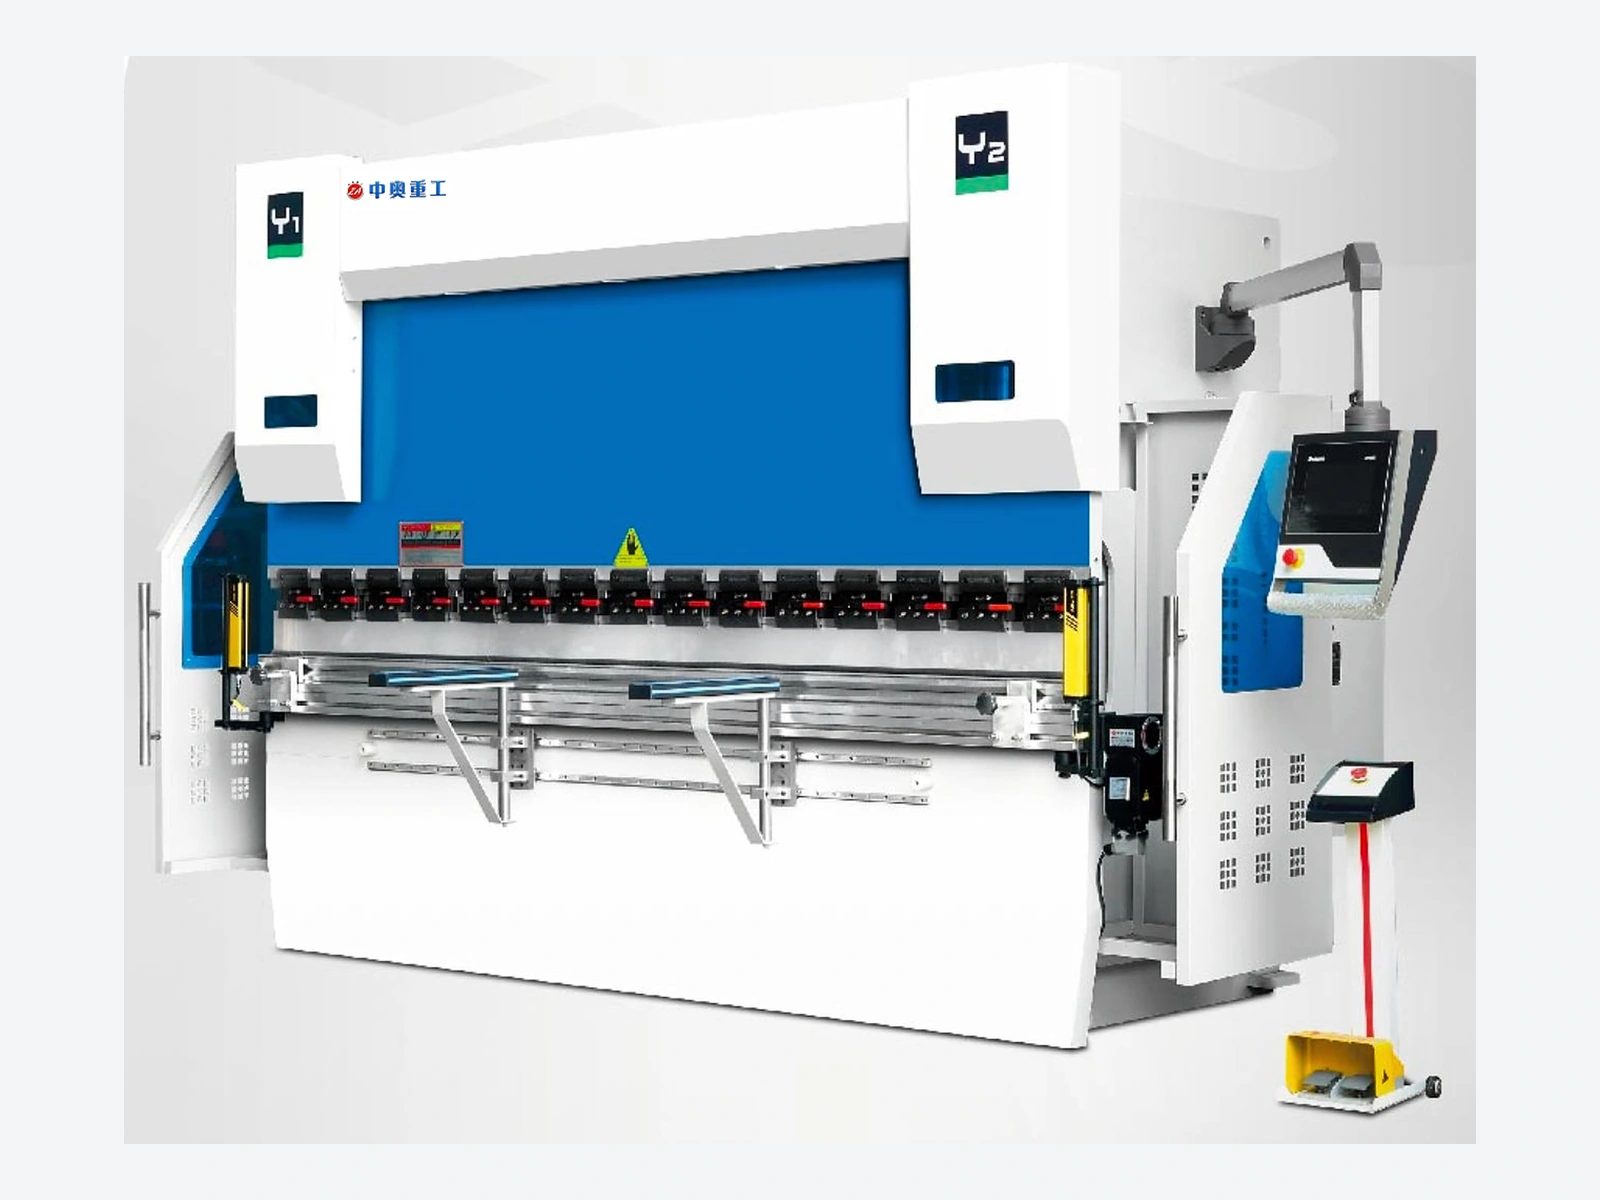
Electro-hydraulic servo bending with configurable CNC control, backgauge and tooling support.
View product
NC hydraulic bending for straightforward sheet metal forming and repeat-part production.
View productShare your material, process, production target and site conditions for a configuration-based quotation.